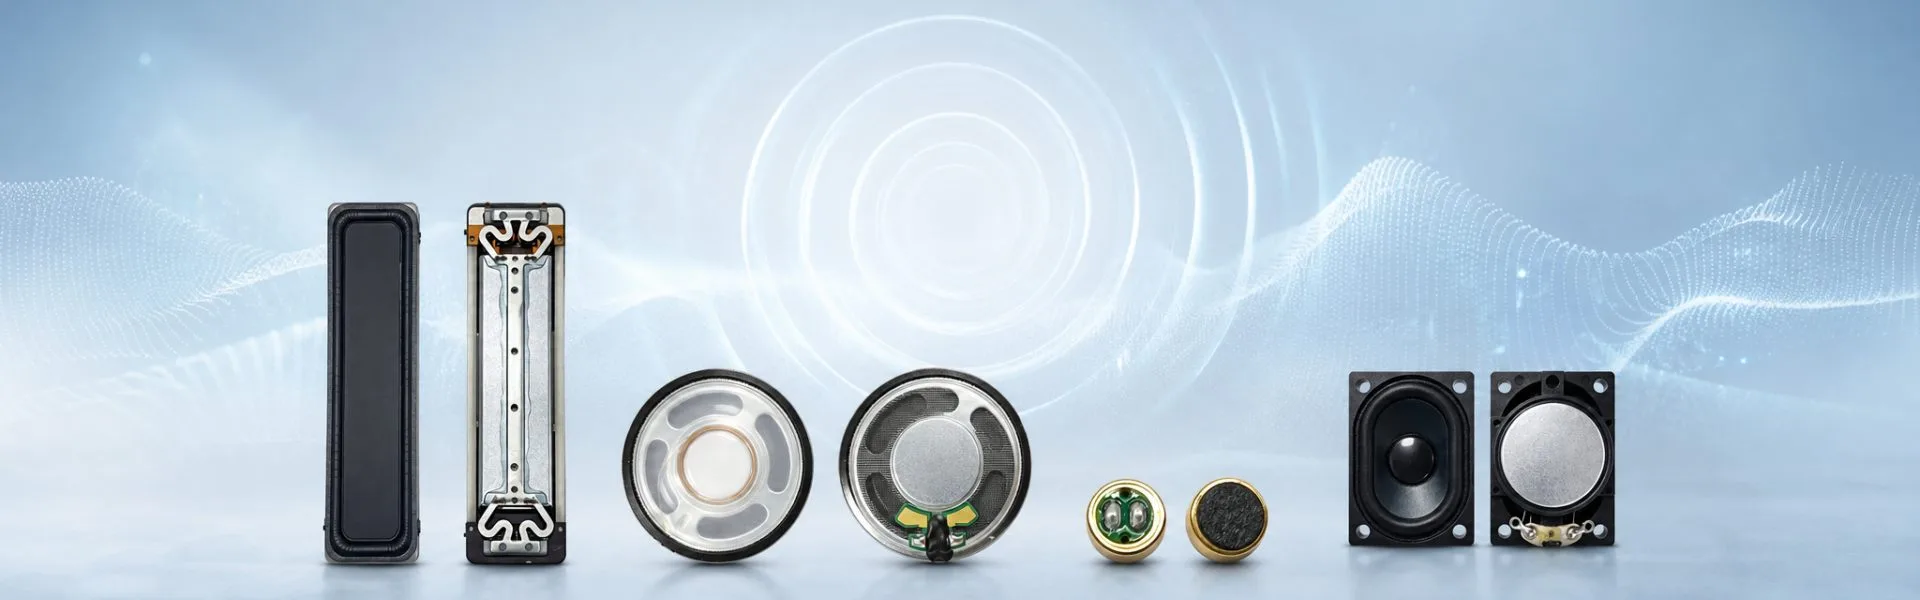
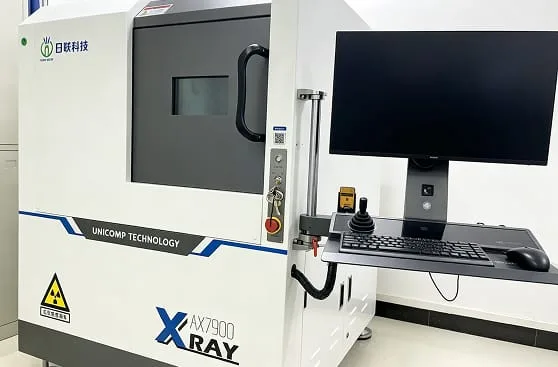
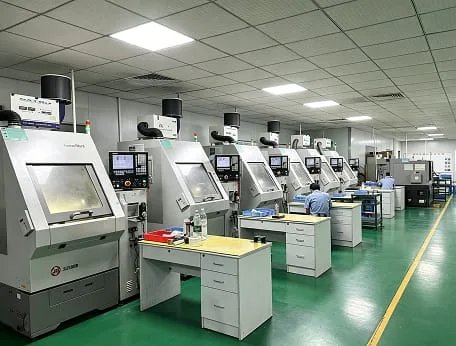
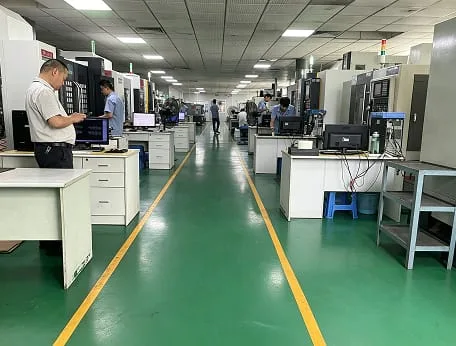
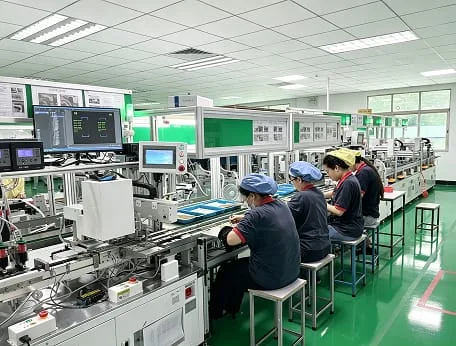
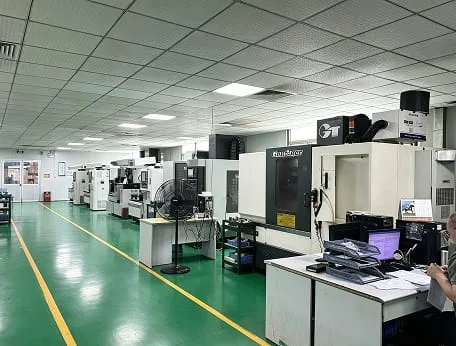
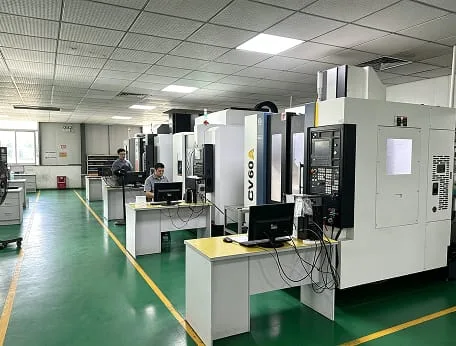
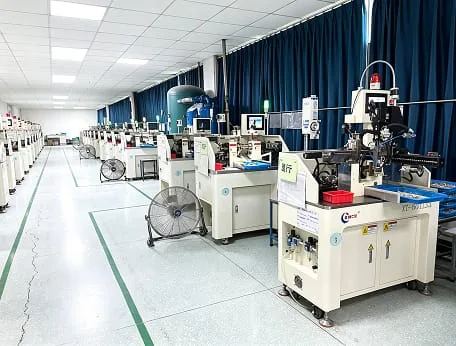
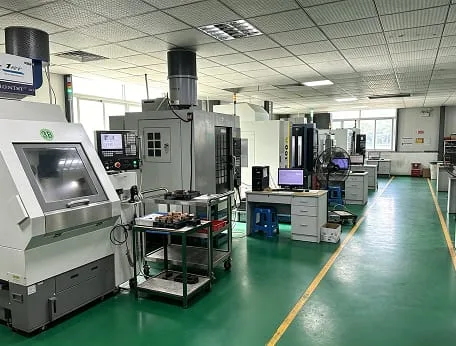
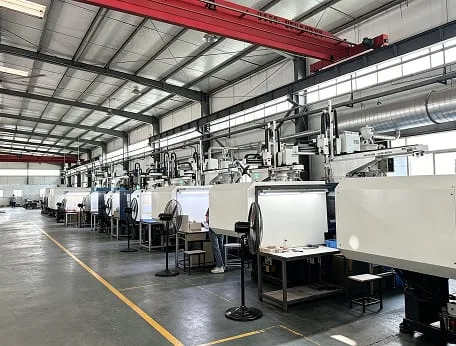
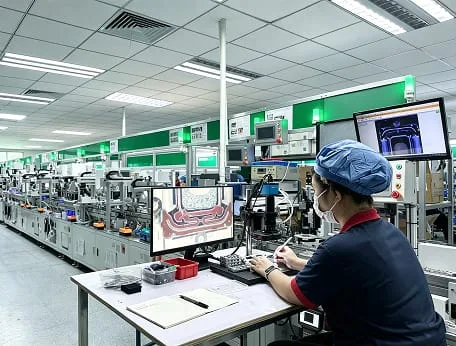
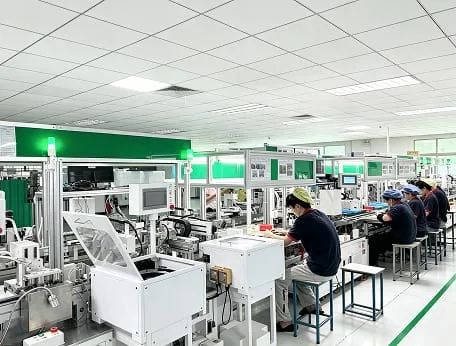
Quality is embedded in every stage of VECO’s design, manufacturing, inspection, and testing processes. Our quality management system is certified to ISO 9001:2015, ISO 14001:2015, ISO 45001:2018, IATF 16949:2016, and QC 080000:2017, together with RBA VAP Silver certification. These certifications provide a structured framework for product quality, environmental management, occupational health and safety, and responsible business practices.
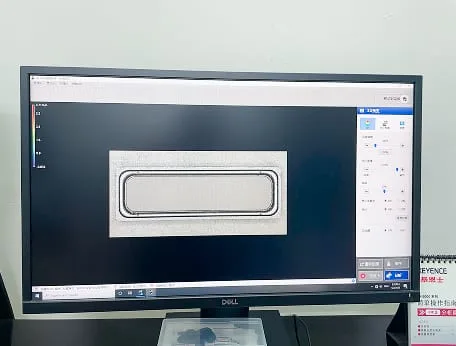
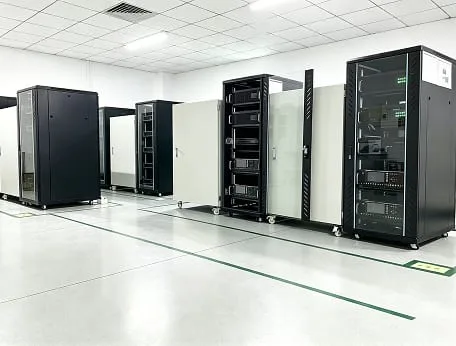
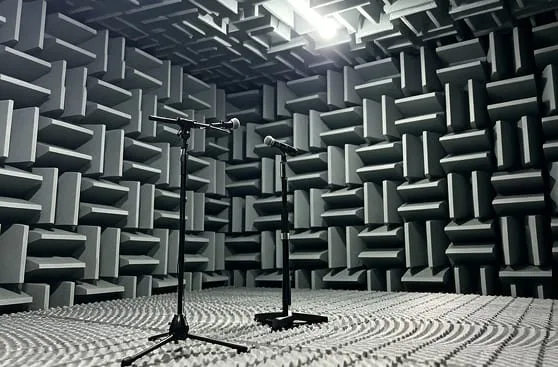
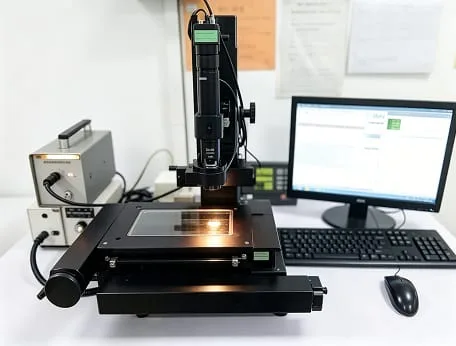
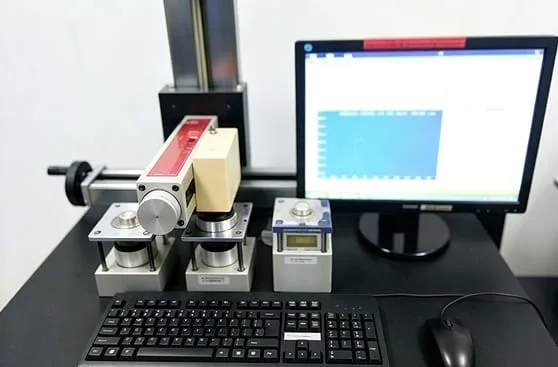
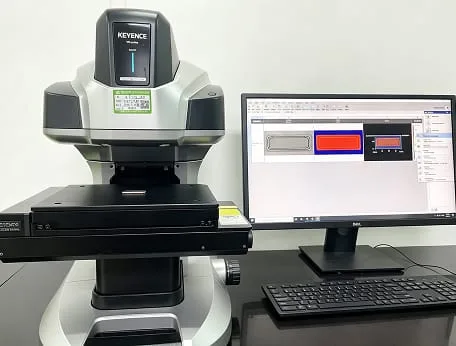
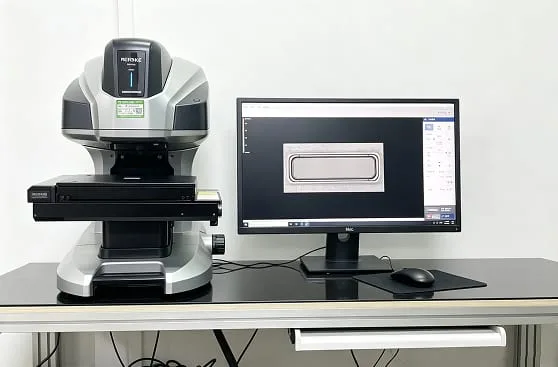
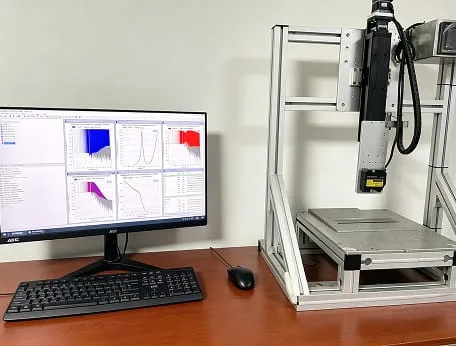
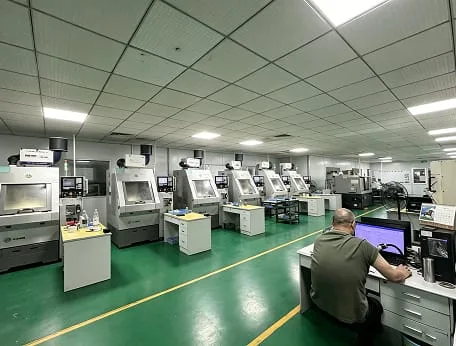
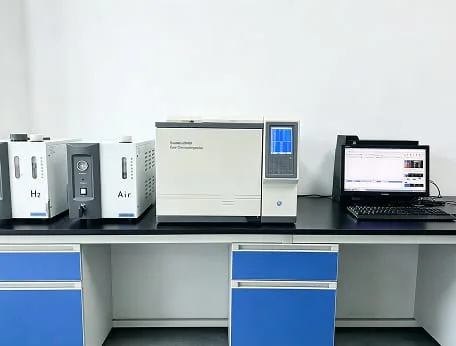
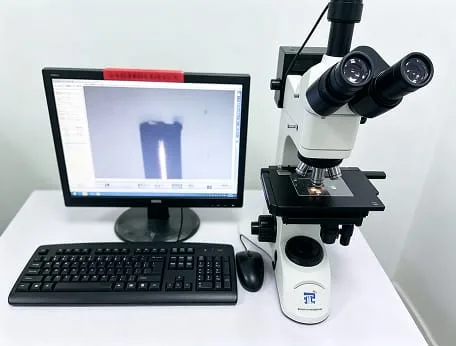
VECO operates professional testing laboratories equipped with advanced acoustic and measurement systems, including Klippel nonlinear measurement systems, B&K audio analyzers, SoundCheck V17, CLIO, Keyence 3D optical measurement systems, and professional anechoic chambers. These capabilities support precise evaluation of acoustic performance, dimensional accuracy, and product consistency throughout development and mass production.
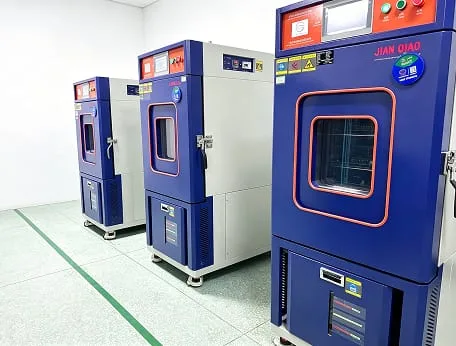
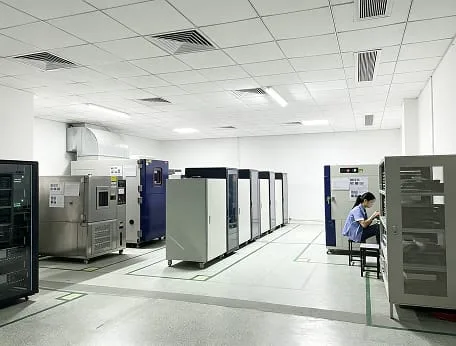
For reliability validation, dedicated environmental testing capabilities cover high and low temperature, damp heat, thermal shock, and vibration testing, allowing products to be evaluated under demanding operating and environmental conditions.
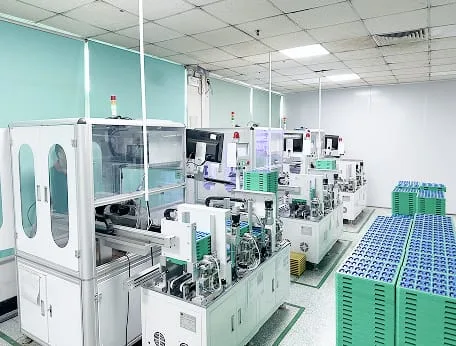
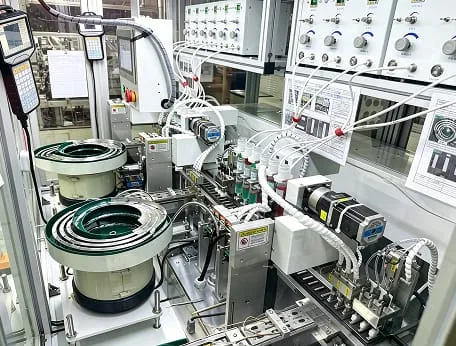
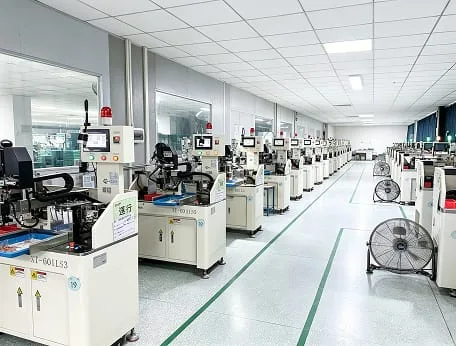
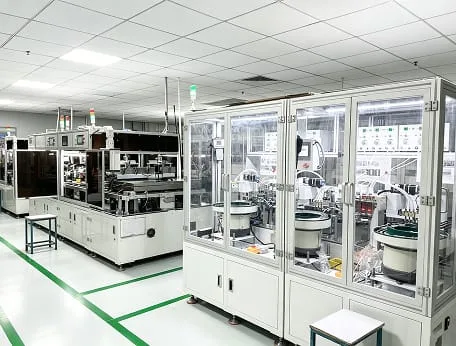
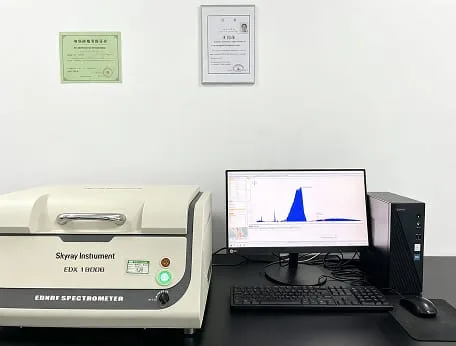
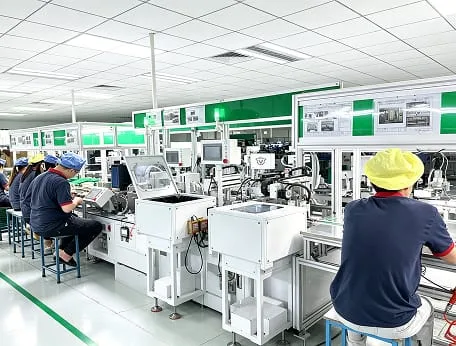
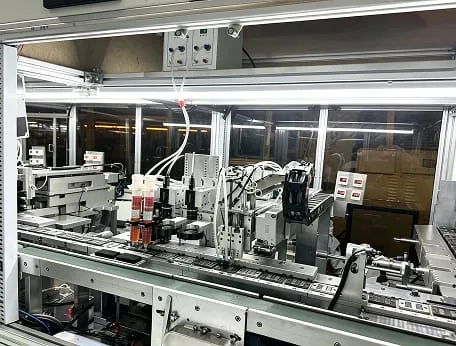
During mass production, 100% acoustic performance verification is conducted using automated CLIO testing systems to ensure consistent performance and compliance with customer specifications. Incoming materials are also inspected using dedicated equipment for RoHS, halogen-free, magnetic field, diaphragm resonance frequency, and 3D dimensional measurement.
VECO is committed not only to product quality, but also to responsible and compliant manufacturing. Our products support applicable global requirements including RoHS, REACH, Lead-Free, and conflict minerals standards, helping customers meet their quality, regulatory, and sustainability requirements.